This article was last revised in 558 Days ago, some of its contents may have changed. If you have any questions, you can ask the author。
From protecting drug purity to achieving nanoscale innovation, cleanrooms are no longer a luxury, but a necessity. Whether you are expanding production scale or pioneering research, well-designed cleanrooms can achieve a return on investment through quality assurance, compliance, and excellent operations.
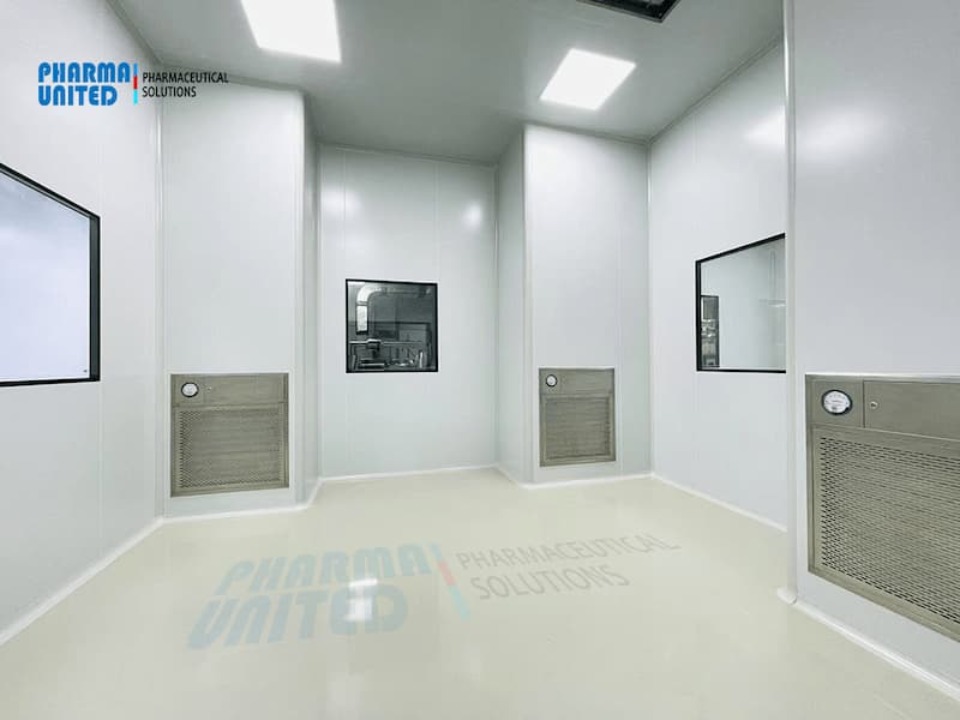
1.Pharmaceutical & Biotech
Application: Sterile filling lines, vaccine production, and lab spaces requiring ISO Class 5-6.
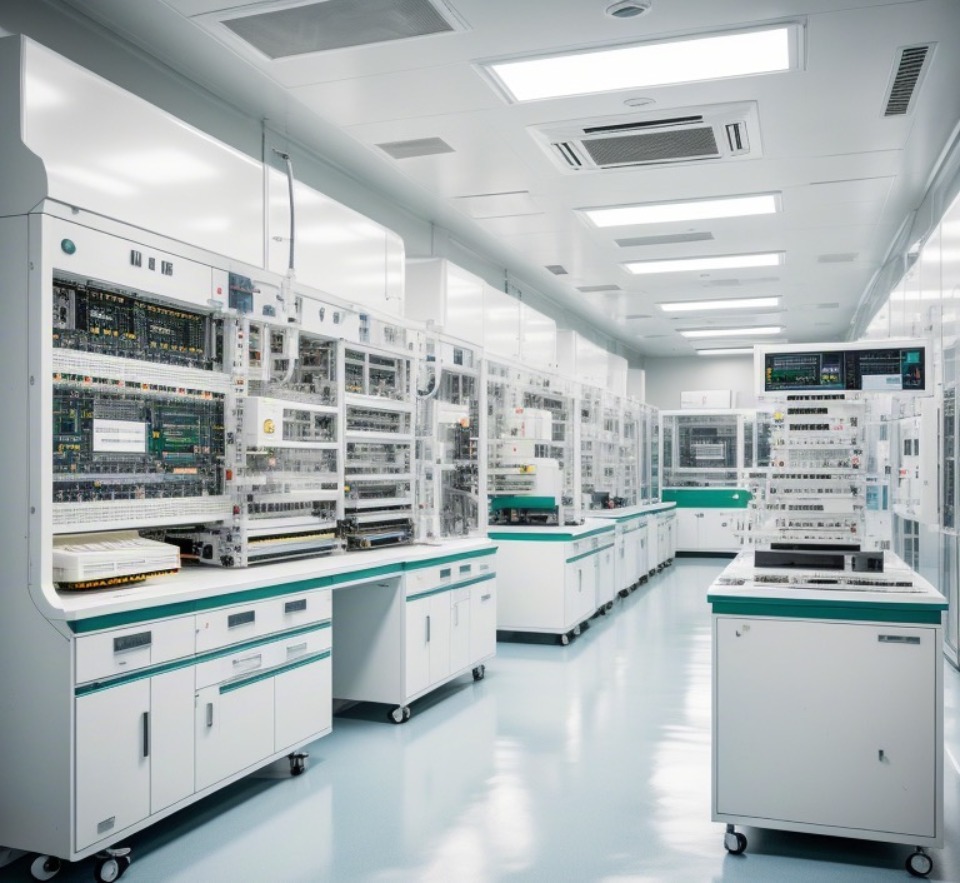
2. Electronics & Semiconductor Manufacturing
Application: Chip fabrication, and nanotechnology research (ISO Class 1–4).
3. Healthcare & Medical Devices
Application: Production of surgical implants, IVD (in-vitro diagnostic) equipment.
4. Food & Nutraceuticals
Application: High-risk food processing (e.g., ready-to-eat meals, probiotic supplements).
5. Research & Academic Labs
Application: University labs, government R&D centers needing flexible, multi-purpose spaces.
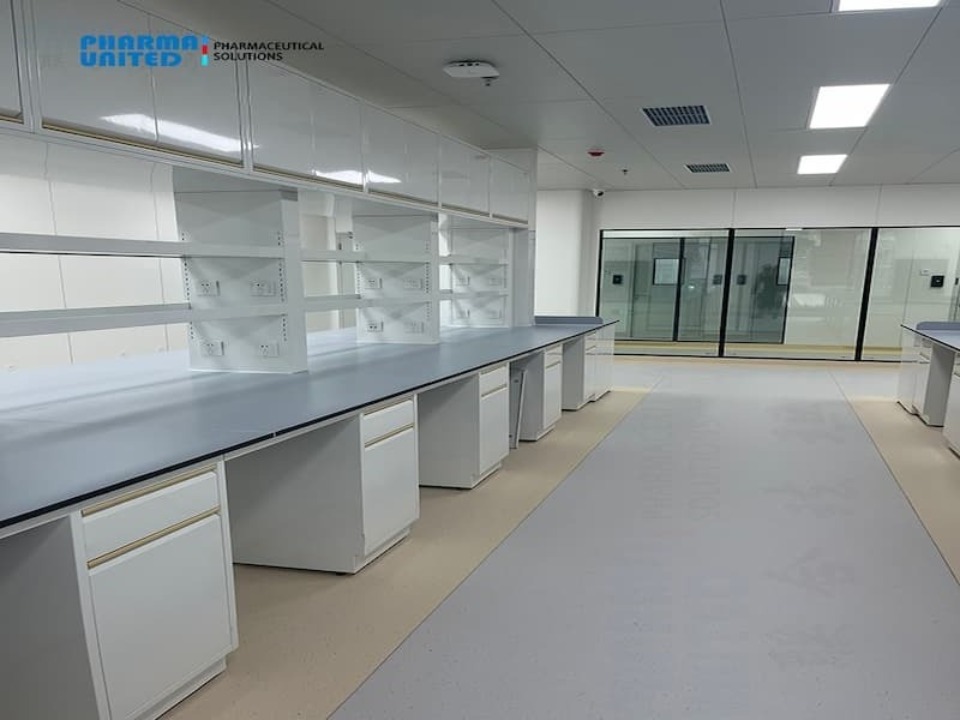
From protecting drug purity to achieving nanoscale innovation, cleanrooms are no longer a luxury, but a necessity. Whether you are expanding production scale or pioneering research, well-designed cleanrooms can achieve a return on investment through quality assurance, compliance, and excellent operations.
Do you need a cleanroom solution? Contact us to plan your project.